Five steps to selecting a cutting tool for your operation
Selection follows the workpiece first, the operation second and the machine third. Work through material, flute count, helix and reach, tip geometry and holder before choosing a SKU.
| SKU | Cutting diameter | Shank diameter | Flute length | Overall length | Corner radius | Flutes | Unit price | Add to cart | |
|---|---|---|---|---|---|---|---|---|---|
| ZY-HP-R0.5x2xD4x50L-2T | 1mm | 4mm | 2mm | 50mm | 0.5mm | 2 | In stock | $4.11 | |
| ZY-HP-R0.75x2xD4x50L-2T | 1.5mm | 4mm | 2mm | 50mm | 0.75mm | 2 | In stock | $4.11 | |
| ZY-HP-R1x4xD4x50L-2T | 2mm | 4mm | 4mm | 50mm | 1mm | 2 | In stock | $4.11 | |
| ZY-HP-R2x6xD4x50L-2T | 4mm | 4mm | 6mm | 50mm | 2mm | 2 | In stock | $4.11 | |
| ZY-HP-R3x9xD6x50L-2T | 6mm | 6mm | 9mm | 50mm | 3mm | 2 | In stock | $8.40 | |
| ZY-HP-R3x9xD6x75L-2T | 6mm | 6mm | 9mm | 75mm | 3mm | 2 | In stock | $11.26 | |
| ZY-HP-R4x12xD8x60L-2T | 8mm | 8mm | 12mm | 60mm | 4mm | 2 | In stock | $14.66 | |
| ZY-HP-R4x12xD8x75L-2T | 8mm | 8mm | 12mm | 75mm | 4mm | 2 | In stock | $17.33 |
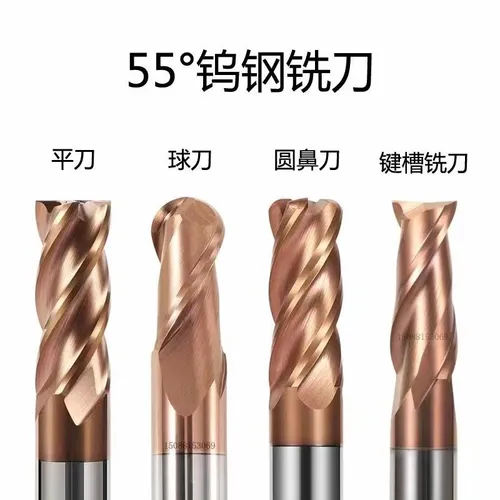
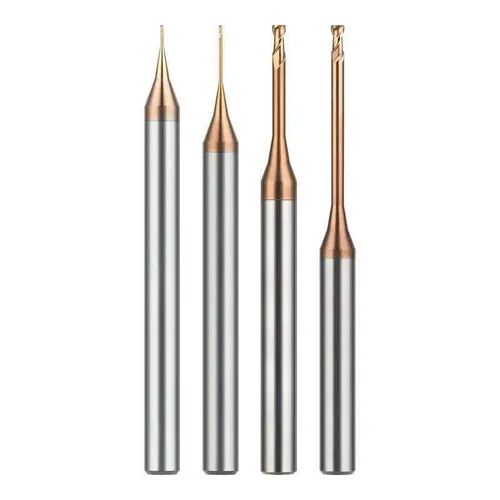
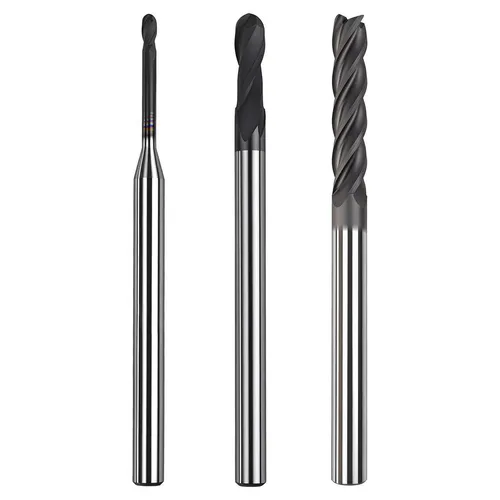
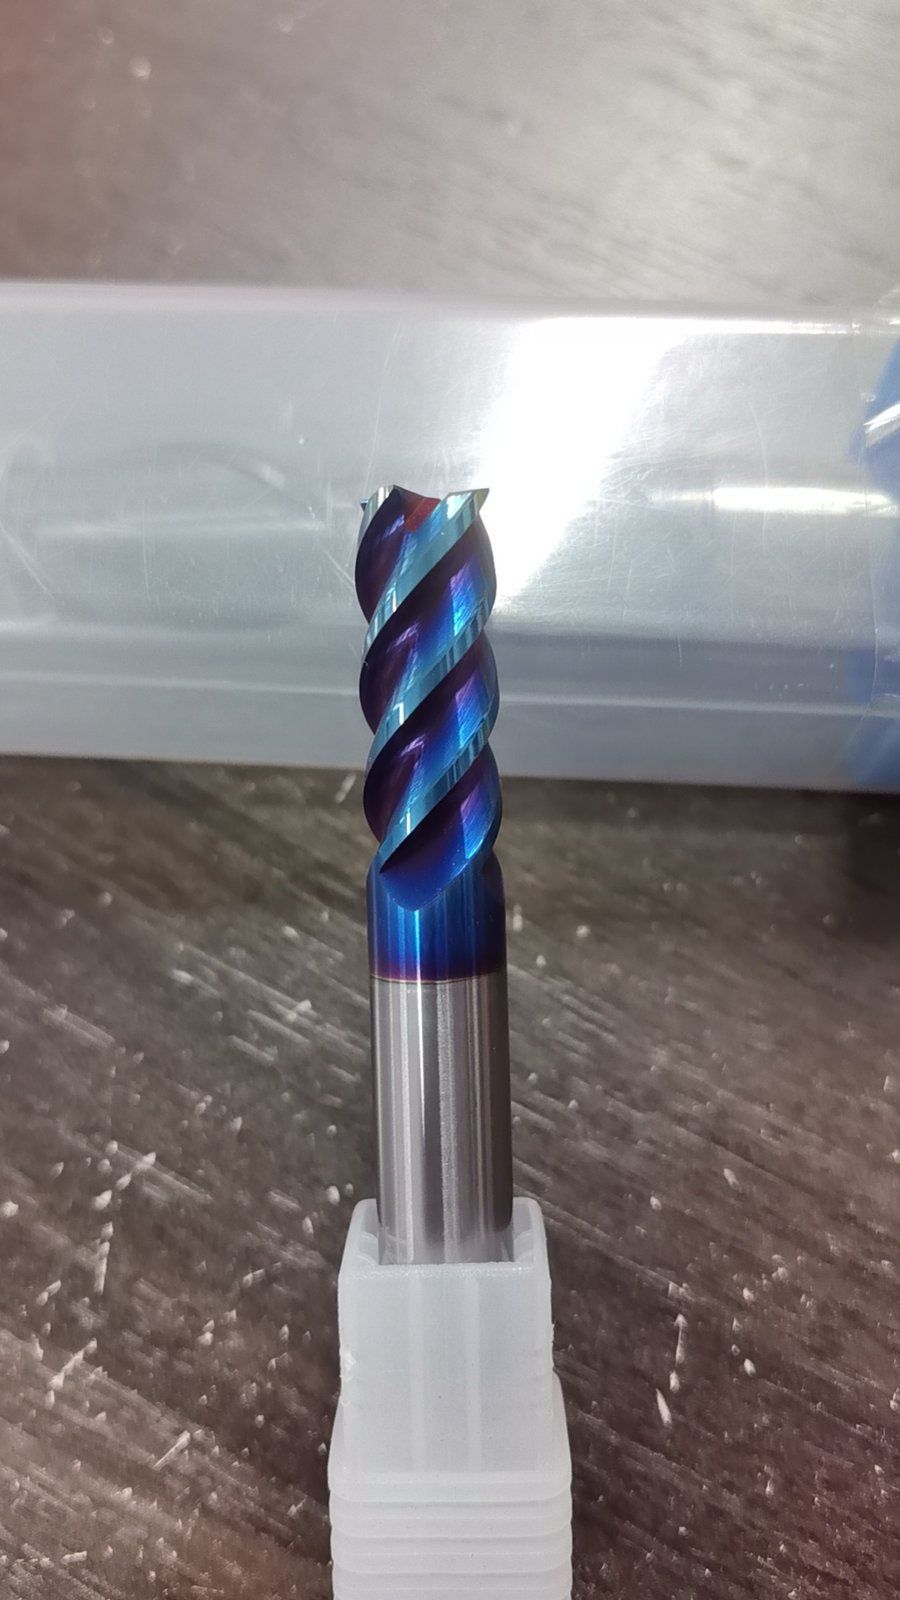
Zhuyi HRC65 nano-blue coated carbide end mill on a fine-grain carbide substrate with high wear resistance and strength, built for high-speed cutting of hard materials. Takes materials below HRC65 from roughing through to finishing in one tool, cutting tool changes and raising machine utilisation. Suitable for A3, S45C, S50C, 40Cr, 42CrMo, 20Cr, Cr12, H13, NAK80, 718 and other mould steels.
Based on 0 reviews
No reviews yet.
Sign in · Sign in to write a review.
Ranges summarize the variants on this page; they do not imply every combination is available. Check dimensions, quantity and material application for the exact SKU. Confirm unspecified tolerances, assembly compatibility and cutting data before ordering.
Selection follows the workpiece first, the operation second and the machine third. Work through material, flute count, helix and reach, tip geometry and holder before choosing a SKU.
Use the workpiece material group and its measured hardness to narrow the tool family, coating and starting cutting data. Always confirm the actual hardness rather than relying on a nominal grade.
Calculate spindle speed from surface speed and diameter, then derive feed from feed per tooth and flute count. Treat every figure as a starting point and adjust against the actual chip, sound and surface.
The catalogue is organised by machining task, so a workpiece and operation can be matched to a category before comparing individual SKUs.
Short answers to the questions that most often block a purchase: which tool, which holder, what to send for a quotation and what happens after delivery.
Match the workpiece, cutting profile and usable reach first. Then compare cutting diameter, shank diameter, flute length and overall length for the exact SKU.